
Derby’s Litchurch Lane workshops have been producing railway vehicles since they opened in the mid-1870s, when the Midland Railway decided it needed a workshop to produce coaches and wagons. Since 2005, it has been the only UK facility able to design, build, engineer, and test trains.
In 2021, it was announced that the works will be part of the production line for 54 HS2 trains as part of a £2 billion order. The works also secured an order for 68 Egyptian monorail trains which was part of a £2.3 billion contract to construct and operate Egypt’s new monorail network. In January 2024, the last of these trains left Derby which is Alstom’s centre of excellence for monorails.
At this time, the works was producing various classes of Aventra units for which there was a production run of 2,660 cars with the last coming off the production line in March 2024. The first Aventra to be built was a Class 345 for the Elizabeth line in July 2016. This was the first of 70 nine-car Class 345 units, the last of which was built in 2019.
Yet, by September 2023, Alstom warned that 1,400 jobs at Litchurch Lane and 900 jobs in its UK supply chain were at risk as production of Aventra units was due to come to an end in March 24. Thereafter, the works had no work in the immediate future. Hence production facilities were to be mothballed, and a redundancy programme was being implemented.
In June 2024, Alstom was eventually given an order for a further 10 x nine-car Class 345 units for the Elizabeth line. This was a £370 million contract which includes maintenance up to 2046. As Andy Butters, the managing director of the Litchurch Lane works, noted: “After a very, very difficult time, this contract gave us breathing space to then seek further opportunities for work.”
This contract was signed very much at the eleventh hour. As the local MP noted, it required: “many meetings, letters, and challenging private conversations with the Secretary of State.”
Thus, the works were reprieved from closure but faced a long pause in production. This required diversification to undertake activities such as component overhaul. It also presented an opportunity for the works to host ‘The Greatest Gathering’ Railway 200 event in August 2025.
Resuming production
Construction of the Class 345 resumed immediately after the Greatest Gathering. On 4 June, Rail Engineer and other members of the press were invited to the Litchurch Lane works to see the roll out of the first completed unit, 345071.
A previous press visit in February, saw the launch of the first of 70 Class 220 units that the works are refurbishing for CrossCountry trains. Next year the works are also to start the refurbishment of 22 Class 222 units before they enter service on ScotRail’s intercity routes. Other future work is the High Speed 2 train order for 54 high-speed trains to be built in a joint venture with Hitachi. In 2023, this was work was expected to start in 2026. It is currently unclear when HS2 train production will start.
Restarting the production lines seven years after the last unit was completed did present some problems. Some components on the first Class 345 build, such as the energy metering and CCTV system, were now obsolete and had to be replaced by new components that required verification by an accredited body. In some cases, new suppliers had to be found.
In addition to the Derby workforce, Class 345 production sustains more than 1,000 jobs in almost 40 UK companies. For example, Time 24 of Burgess Hill has the contract to supply the wiring looms which make up to 50 miles of wiring in each train. Some large components come from outside the UK. For example, the Chinese Qixing Group supplies bodyside panels and aluminium extrusions. Bogies are supplied by Alstom’s Siegen bogie plant in Germany which was described in Issue 216 (Sep-Oct 2025) as part of our report on the IMechE’s 2025 technical tour.
Unlike most other rail manufacturers whose train production involves fitting out a welded bodyshell, Alstom uses a Complete Knock Down (CKD) method of rail vehicle construction which is akin to an IKEA flat pack. This fits out the roof and underframe which can then be turned upside down for ease of assembly before the car body is assembled. CKD requires the car body parts to be bolted together as the car assembly is an integral part of the fit-out process. This requires around 3,500 huck bolts for each car. The use of bolts also eliminates risk of heat distortion and reduces the risk of fatigue cracks.
An essential and sometimes troublesome aspect of new trains is their software, in particular the Train Control Management System (TCMS). This controls every aspect of the train including train radio, passenger information system, brake, auto-coupler, CCTV, heating ventilation air conditioning (HVAC), doors, platform identification beacon system for selective door opening, and signalling systems. The Class 345 trains have to change between three different signalling systems: AWS/TPWS, CBTC, and ETCS.
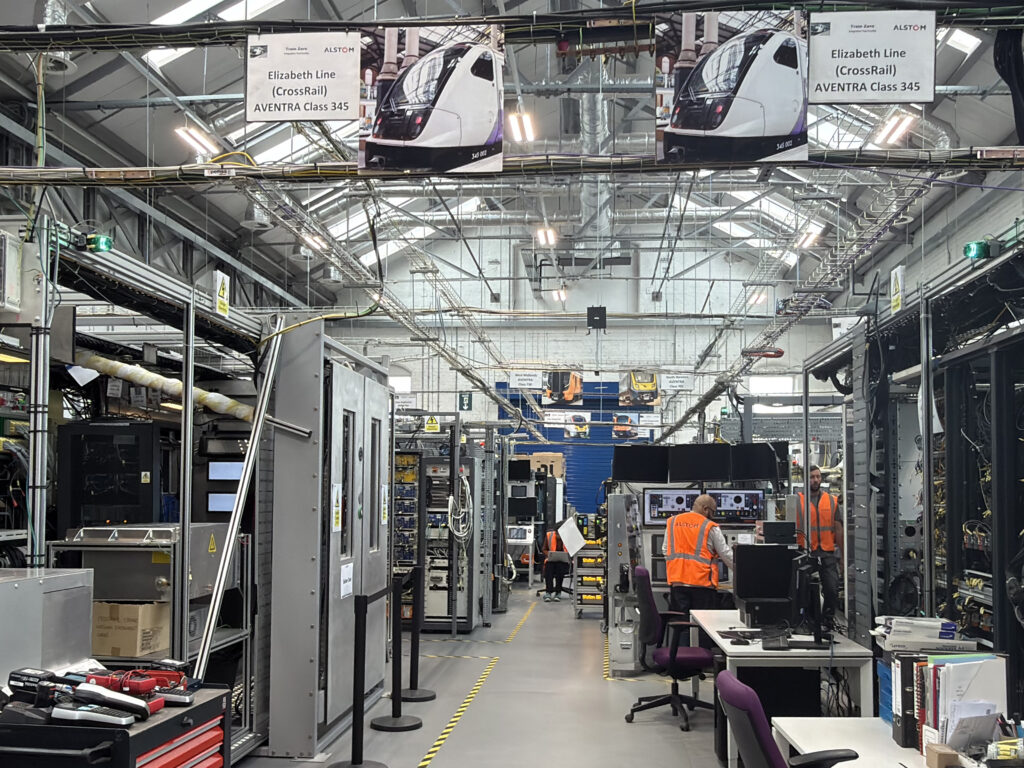
As with all software there are updates which, if not thoroughly tested before implementation, can introduce latent faults. The Litchurch Lane works manages this issue in its ‘Train Zero Deliveries’ (TZD) workshop. This has static test rigs of all the electronics and components of all types of Aventra units to simulate how the train’s software and hardware work together.
This offers significant benefits for train design, software development, systems integration, and test verification as it enables more thorough testing to be done than is practicable on a train. Once trains are in service it is an essential part of the validation of the train software updates. While visiting the TZD workshop, the large volume of electronic equipment on a modern train was evident which is something that is not obvious to passengers.
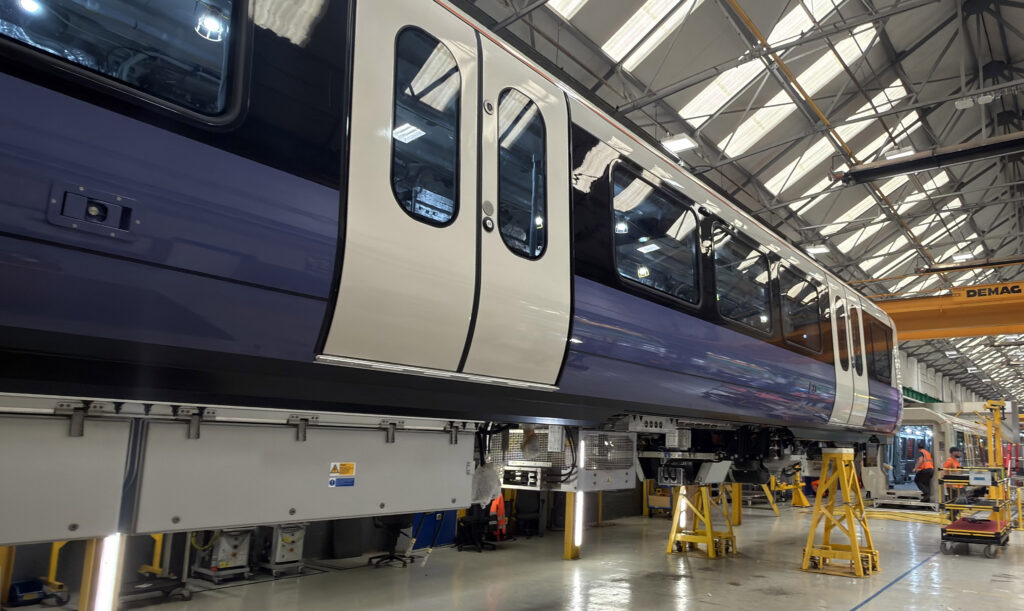
Production line
The five-stage assembly of the Class 345 units takes place in the 10,000 square metre U-shop which is 176-metres long and was built in 1910. This shop welds together aluminium extrusions and components to manufacture roof panels and underframes for the production line. This has a five-stage assembly process as shown below.
Stage 1 – Roof sub assembly: The roof panel is mounted in a rotating jig for easy installation of cables, ceiling modules, lights, door mechanisms, pantographs, and HVAC units.
Stage 2 – Underframe sub assembly: The underframe is placed upside down for the installation of traction motor ducts, brake reservoir tanks, pipework, high and low voltage cables, and bolsters.
Stage 3 – Car body assembly: Roof, underframe, and bodyside panels are held in a ground-level jig where they are bolted together. Floorplates are then installed together with thermal and acoustic insulation, interior panels, doors, and windows. Driving cabs and intermediate car body ends are also bolted in place. This stage has a rig of travelling water jets to confirm that the completed car body is watertight.
Stage 4 – Underframe equipment: while the car body is on a raised stand, underframe pipework, battery rafts, power converters, couplers and energy absorption are installed.
Stage 5 – Completion – the car body is lowered on its bogies and seating is installed.
Each of these stages takes 3.5 days. The completed individual cars are then transferred to V-shop where they are coupled to form a train for static testing. V-shop is a 10,000 square metre testing and commissioning facility which was opened in May 2016. At 250 metres long it can accommodate the 204-metre-long nine-car Class 345 train sets.
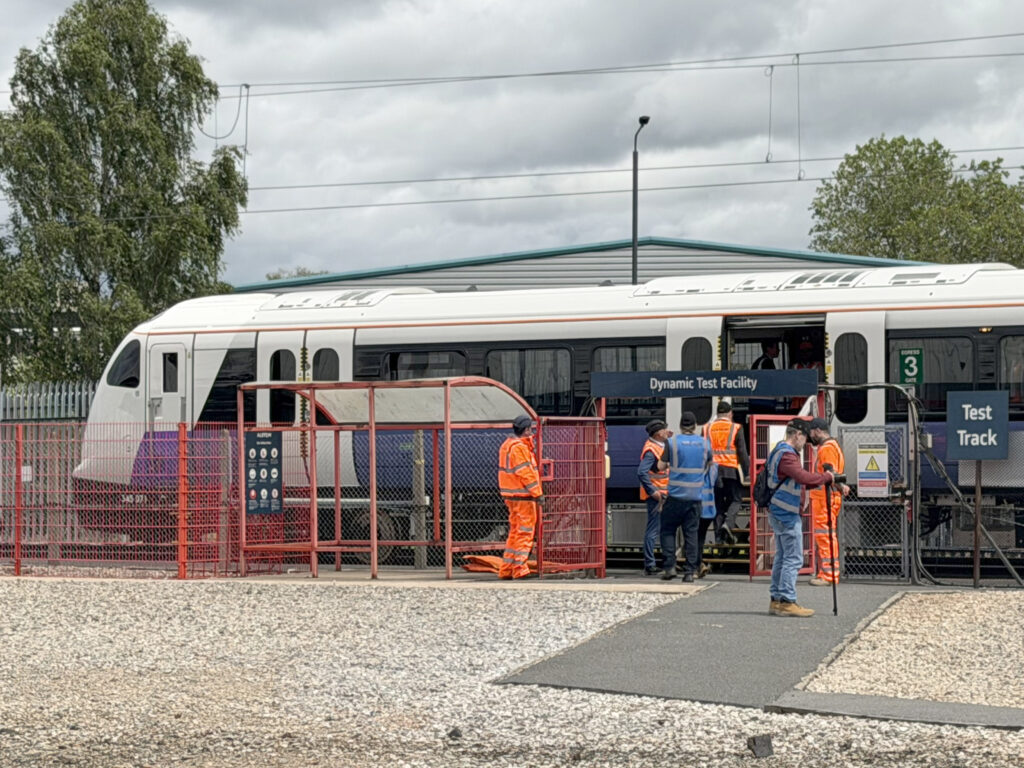
Test track then London
On the test track the press party had the opportunity to ride on Unit 345071 which was the first completed train of the new order. The Litchurch Lane test track opened in 1989 and is 1.4km long with 25kV AC overhead line equipment and 750V DC third rail.
The functionality of all train systems can be tested on this test track up to a maximum speed of 63km/h. Train testing typically requires 50km of running on the test track before units are released from the works. They are then hauled from Derby to London by Direct Rail Services using a locomotive that has a brake enabled coupler to enable the Class 345 unit’s brakes to be operational during this journey.
A YouTube video shows that 345071 arrived in London on 14 July. There was something distinctly incongruous about the sight of a 60-year-old Class 37 locomotive hauling on a state-of-the-art Elizabeth line.
On arrival at the Elizabeth line’s Old Oak Common depot, the unit will have to complete 2,400km of fault free running before it can enter passenger service. As the new Class 345 build units are functionally identical to the original fleet, there is no requirement for driver training or type approval.
Hence, 345071 should enter passenger service in a few months’ time. It is expected that all the new Class 345 units will have entered service by the end of 2027. By this time, it is expected that these additional units will be used to increase the frequency of Elizabeth line services. Transport for London and Network Rail are currently discussing the required timetable options for this.
Since the central core of the Elizabeth line opened in May 2022, 850 million journeys have been made with many trains full and standing. A more frequent timetable, made possible by the additional 10 Class 345 units, is therefore much needed to boost capacity ahead of the opening of High Speed 2’s Old Oak Common station. With the additional trains, the 80-unit Class 345 fleet laid end-to-end would be over 16km long.
In this way these new trains will deliver real economic benefits by improving London’s transport while also supporting skilled jobs in Derby and its nationwide supply chain.
Image credit: David Shirres